6″-300LB 2 Piece Cryogenic Floating Ball Valve
Description
Technical Data Sheet: 6″ (DN150) Class 300 Cryogenic Floating Ball Valve
1. General Description
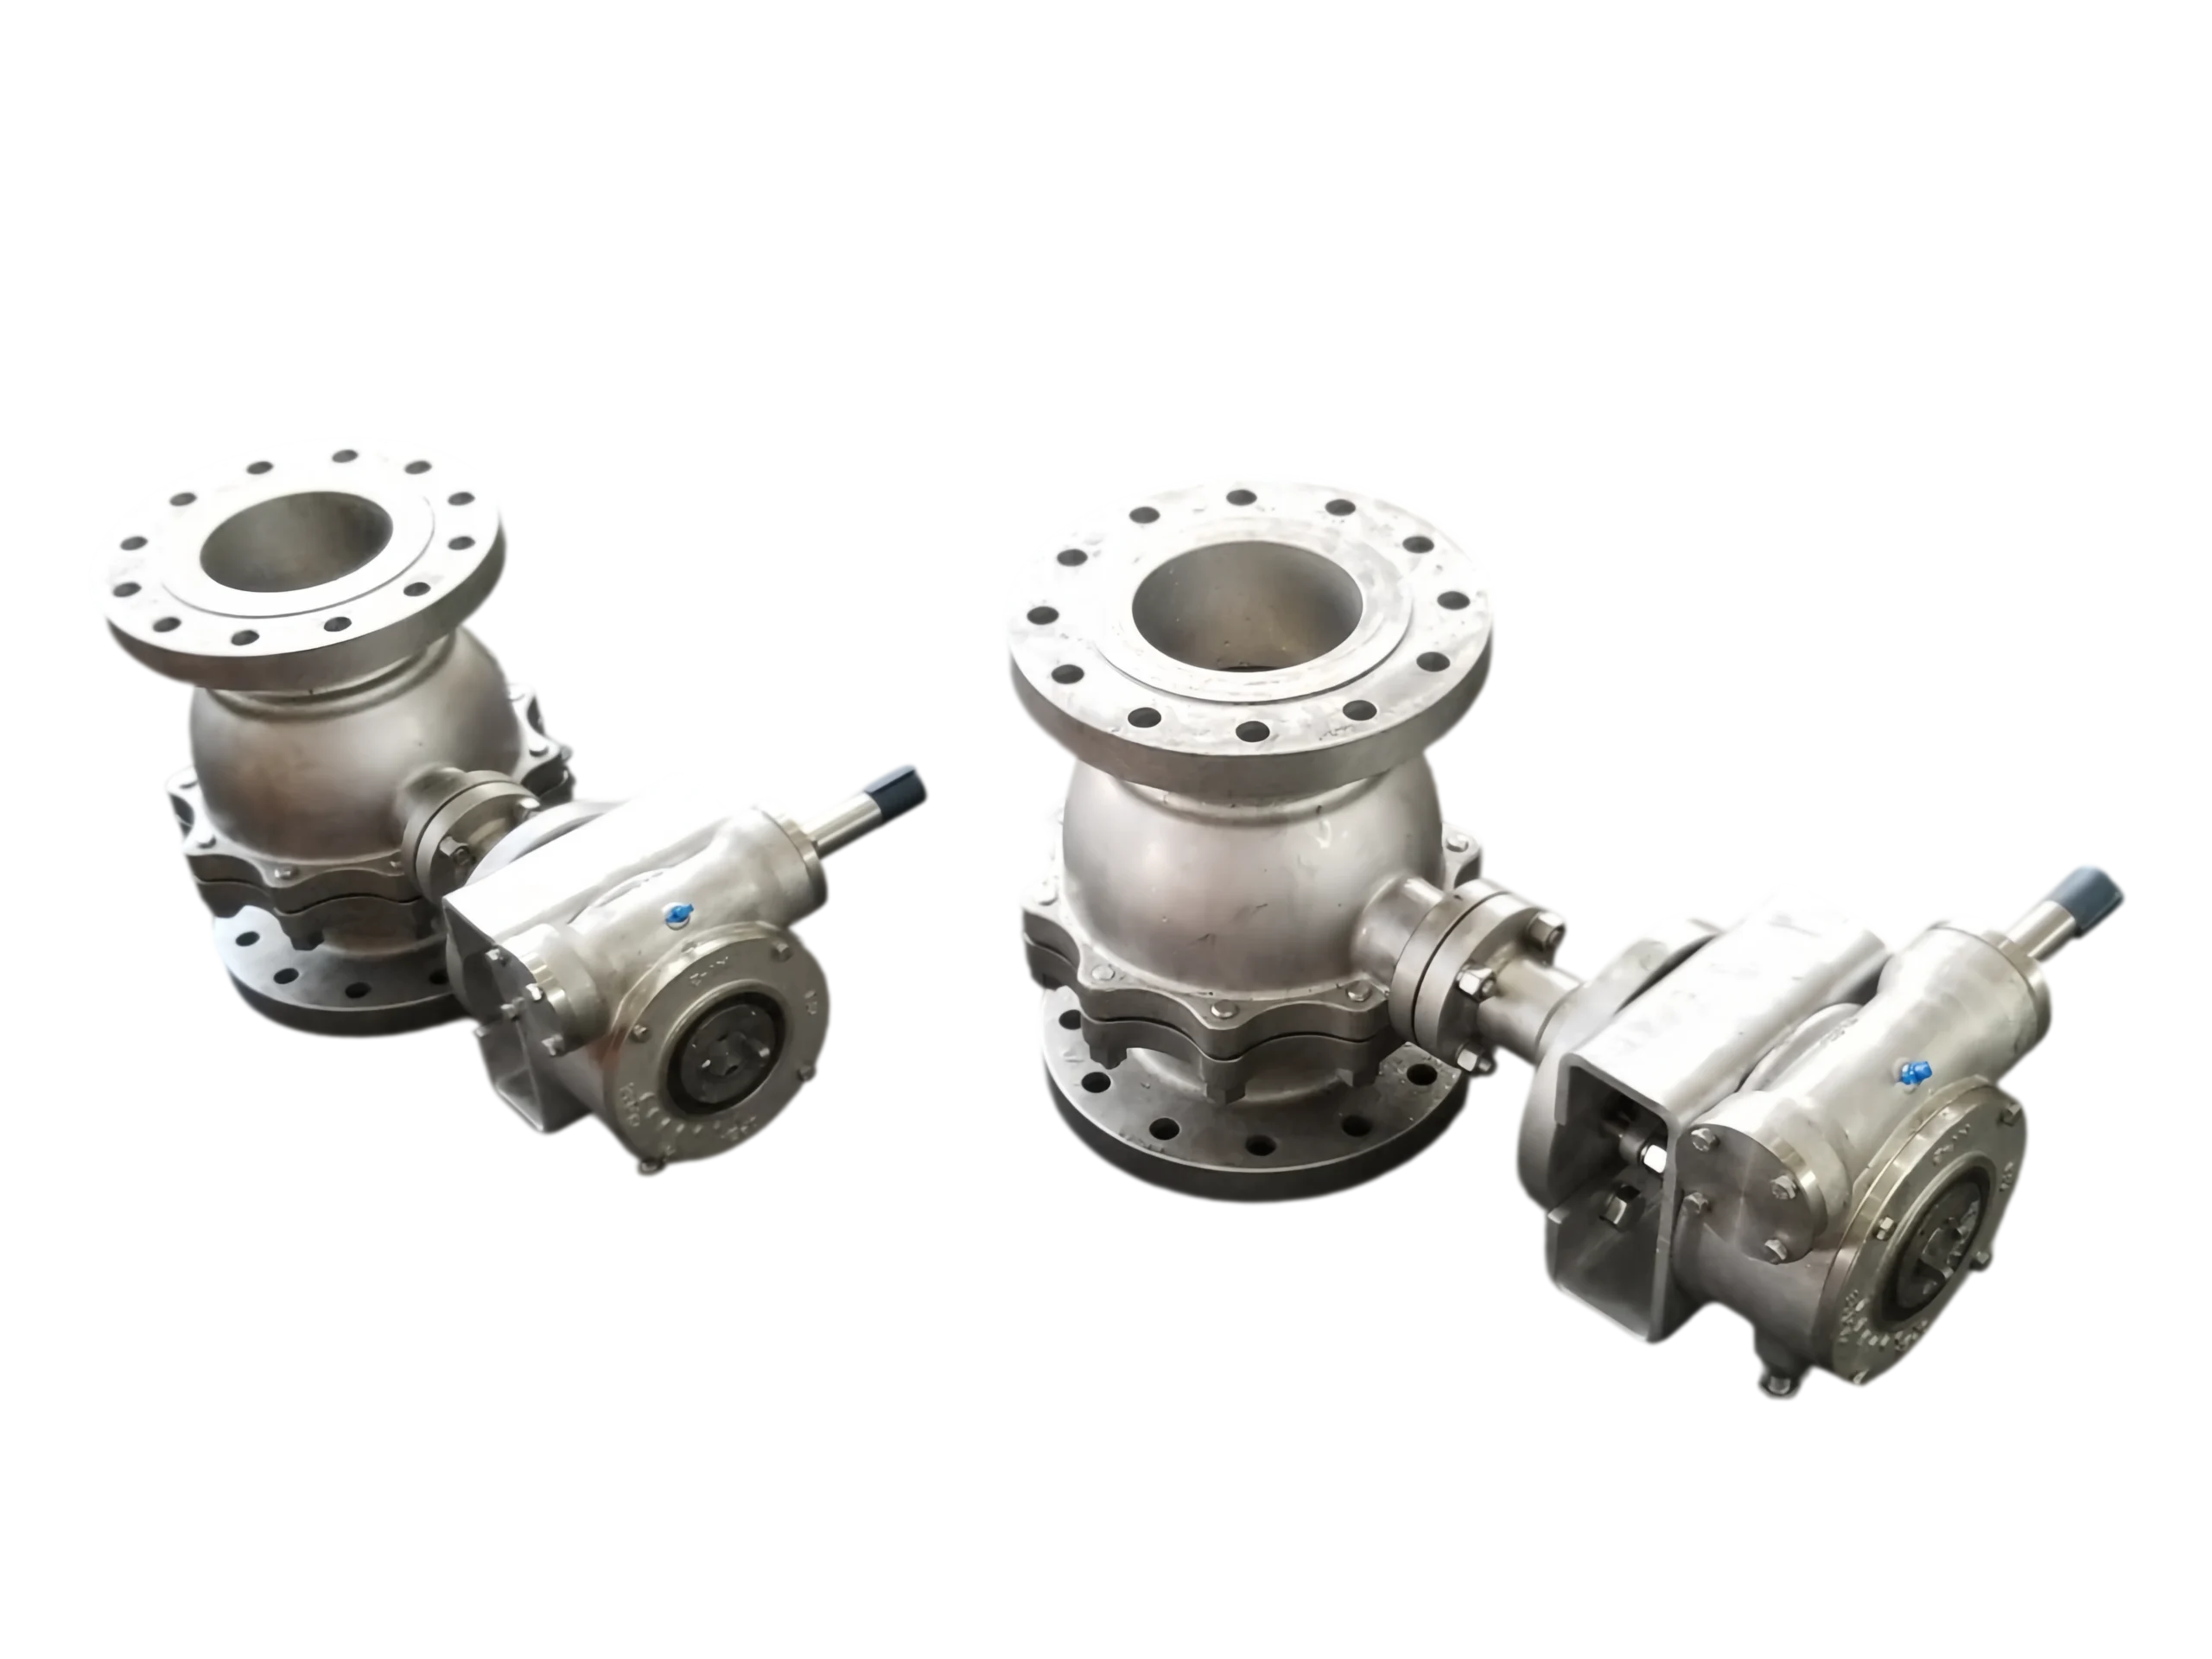
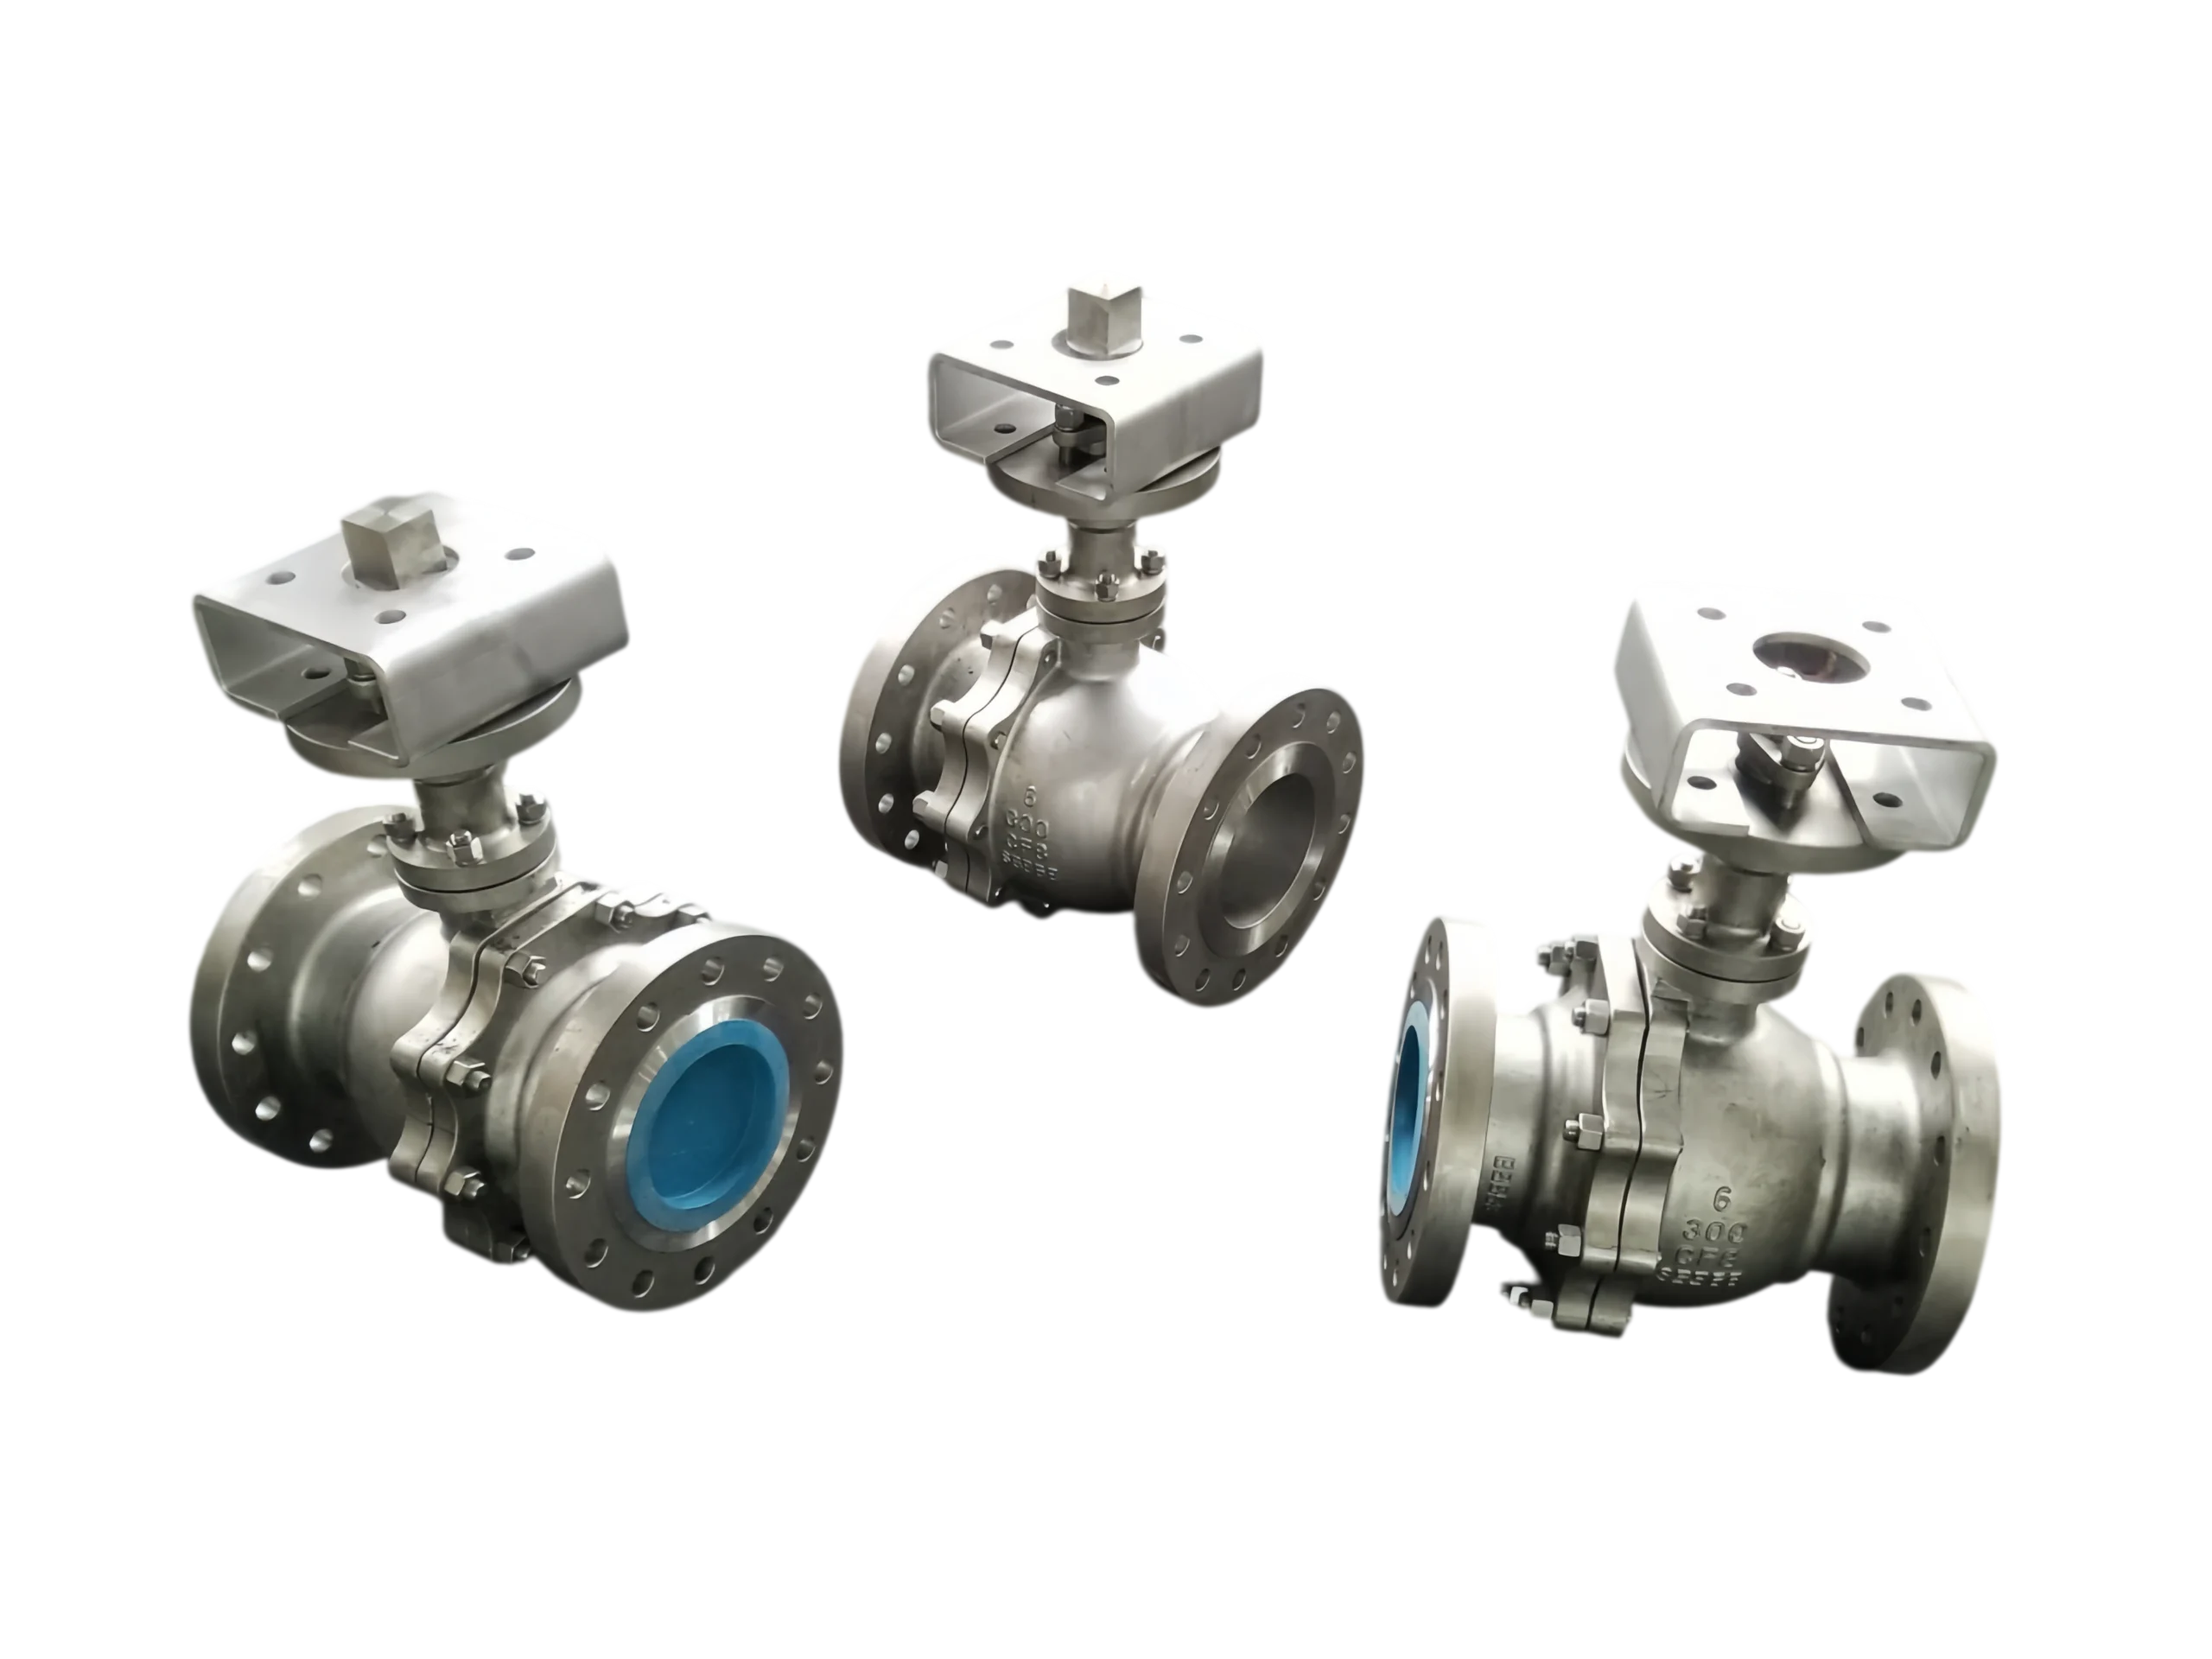
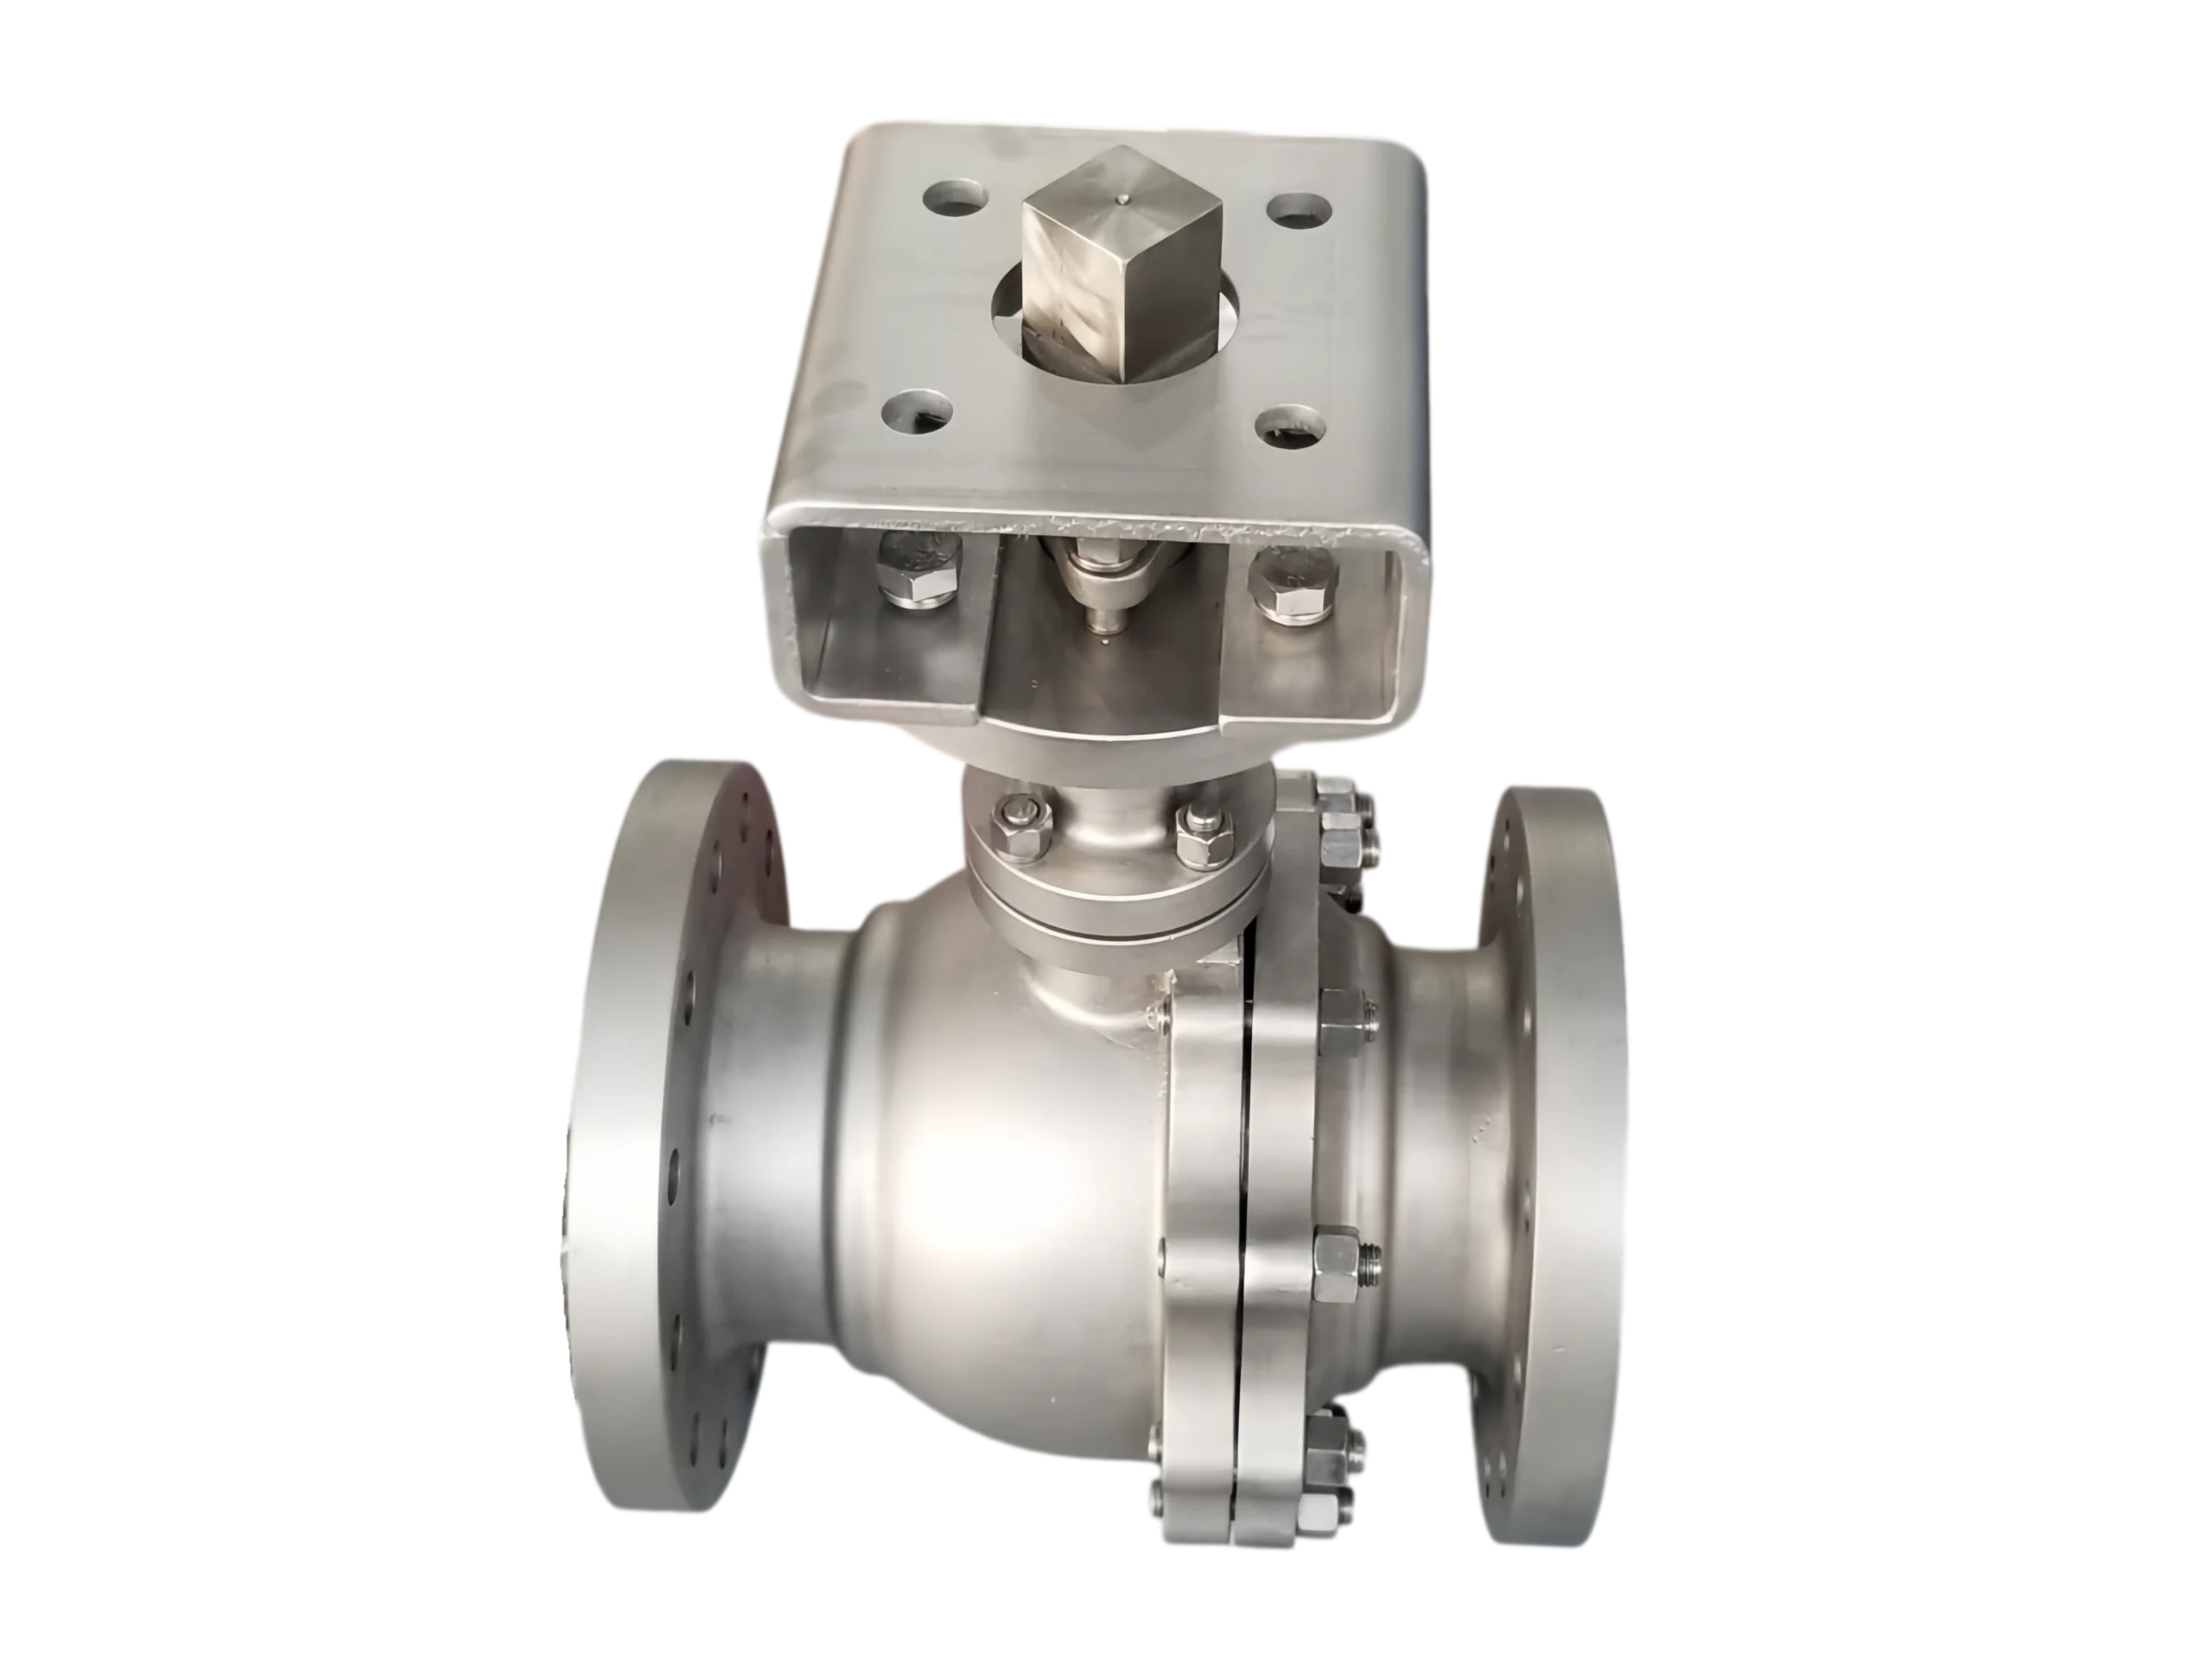
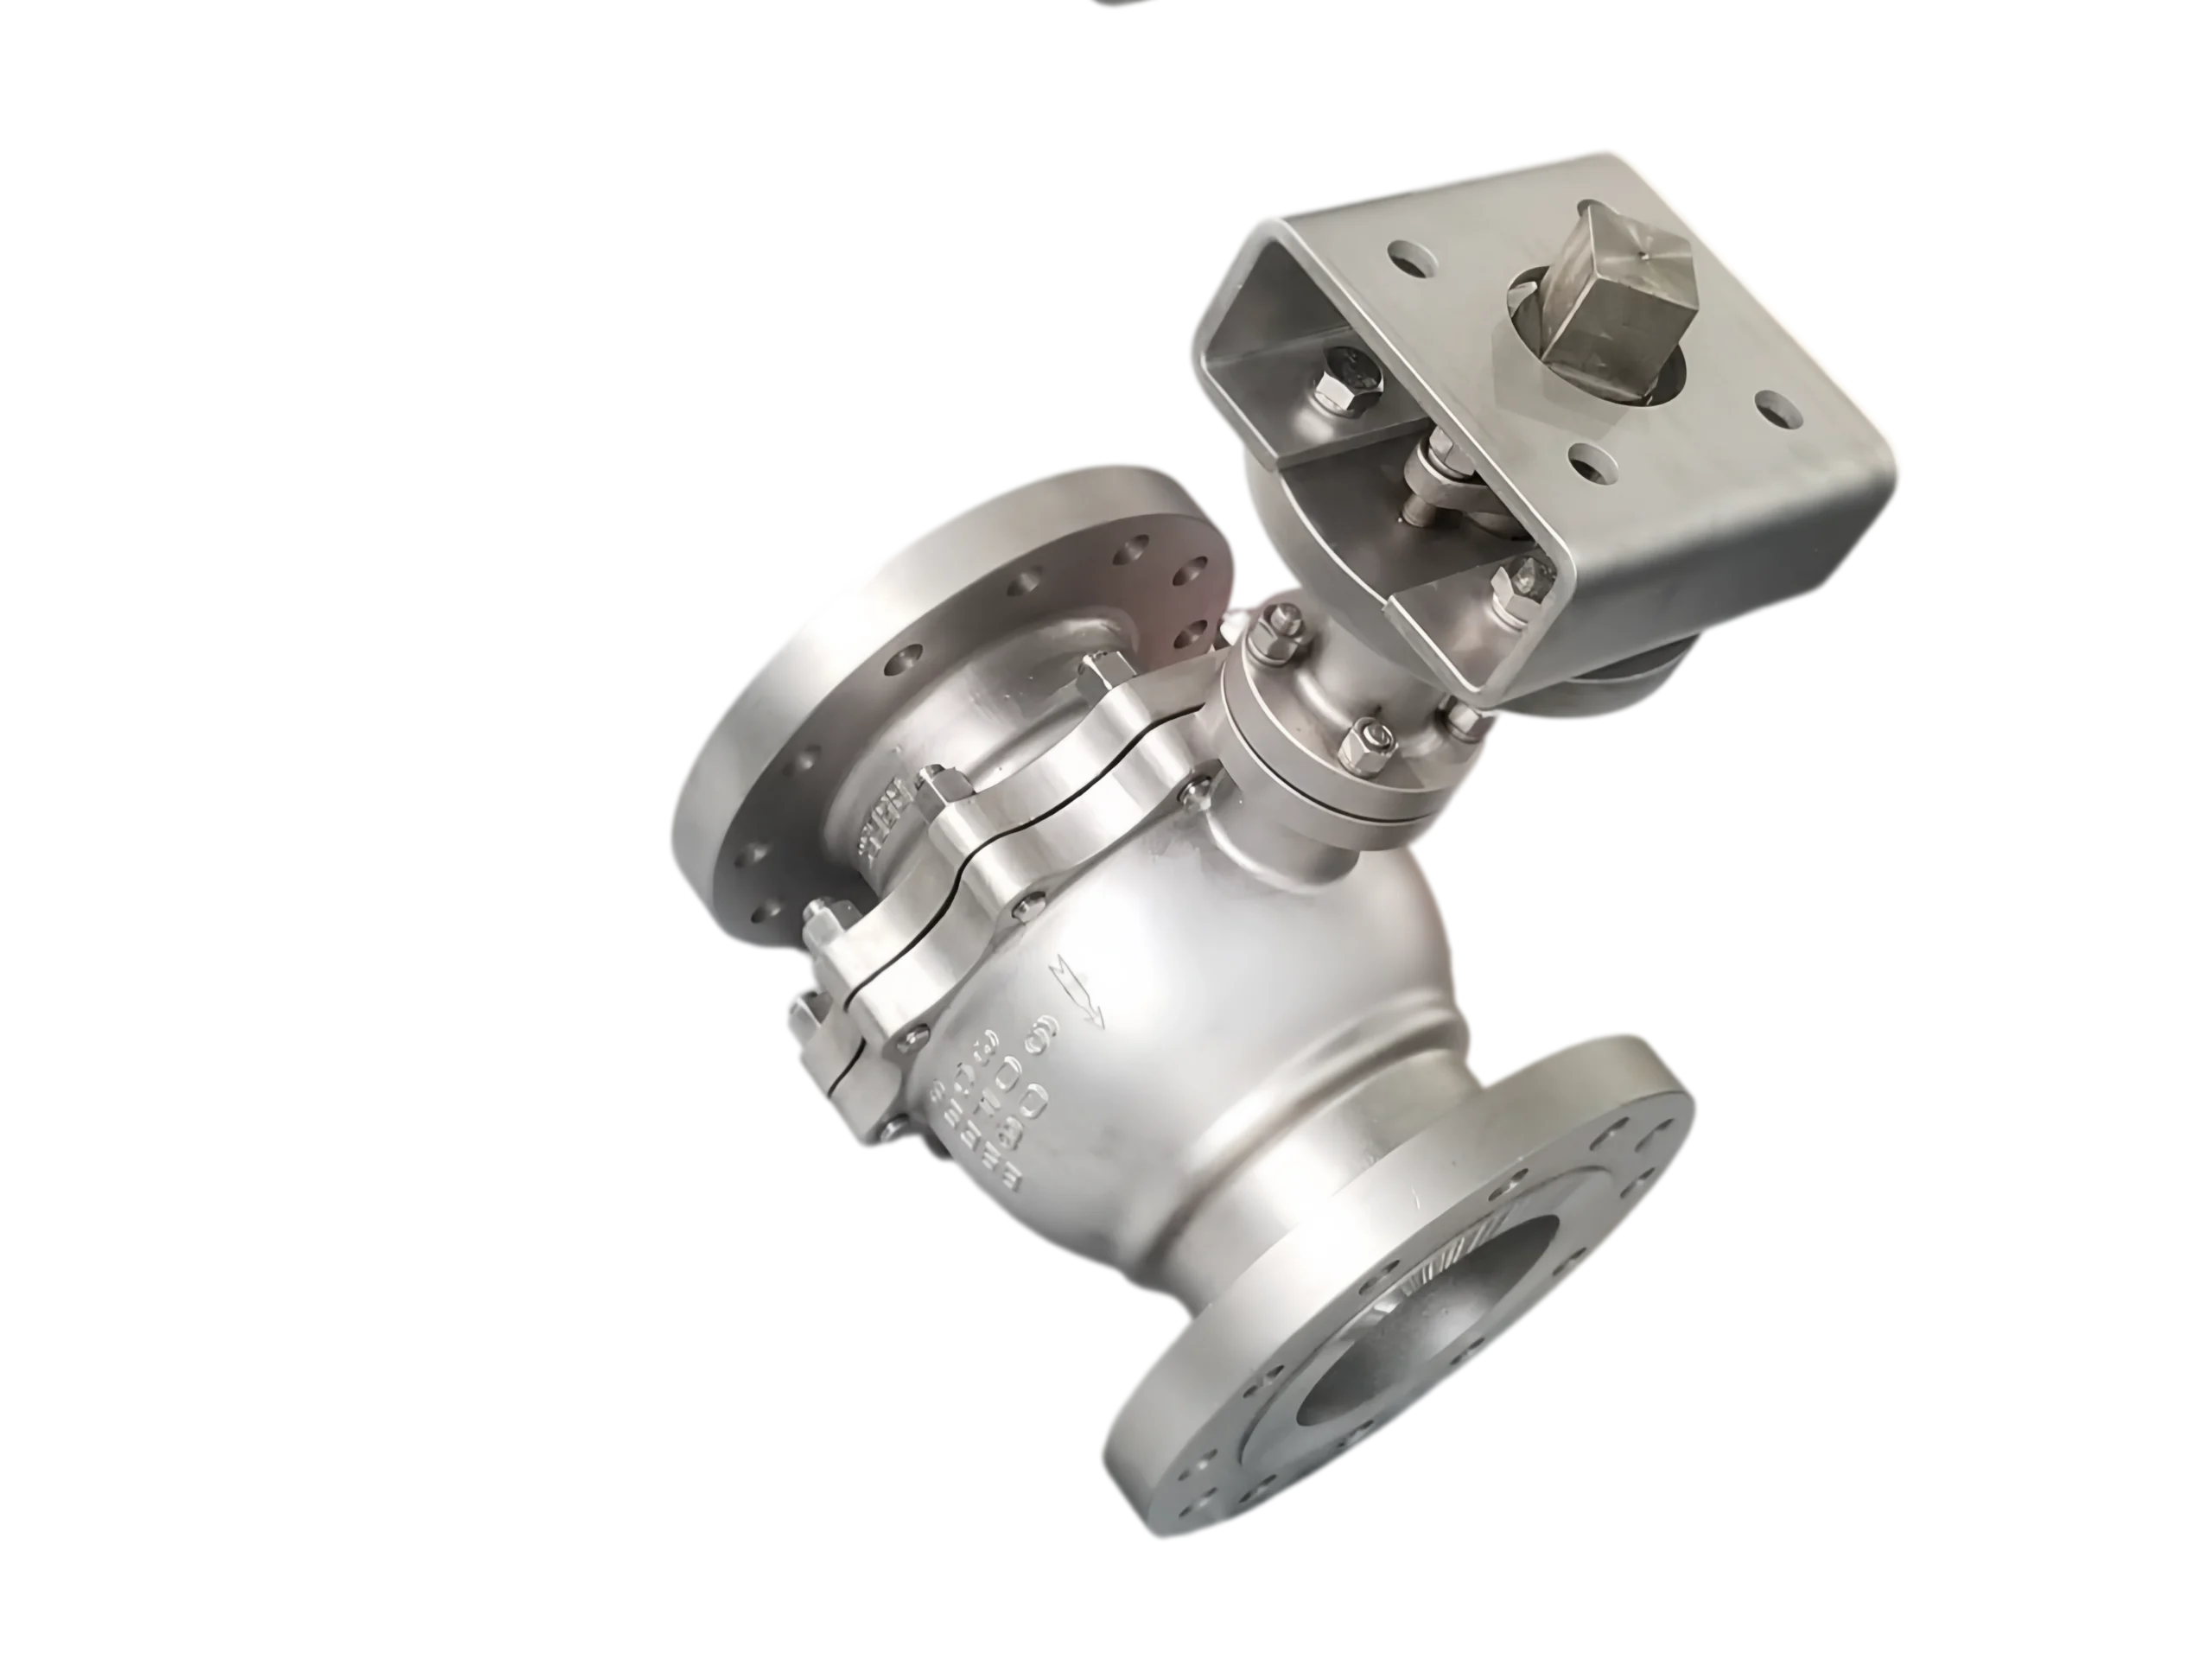
This data sheet covers a 6-inch (DN150) Class 300 cryogenic floating ball valve with a two-piece, side-entry flanged body and extended bonnet design. The valve is precision cast from ASTM A351 CF8 stainless steel and is specifically engineered for low-temperature and cryogenic service down to -196°C. It features a PCTFE (Polychlorotrifluoroethylene) seat for reliable sealing at cryogenic temperatures, a manual gear operator for reduced operating torque, and an ISO 5211 top mounting pad for straightforward actuator integration.
The extended bonnet design is a critical feature that keeps the stem packing and gland away from the cryogenic media, ensuring the packing operates above 0°C and preventing seal failure due to low temperature.
2. Nameplate Data (Confirmed from Images)
| Parameter | Value |
|---|---|
| Nominal Size | 6″ (DN150) |
| Pressure Class | 300LB |
| Body Material | CF8 (ASTM A351) |
| Traceability Code | T2540 / T2538 (Cast on body) |
3. Design Codes & Standards
| Item | Applicable Standard |
|---|---|
| Basic Design | API 608 / API 6D / ISO 17292 |
| Cryogenic Design | BS 6364 / ISO 28921-1 / MSS SP-134 |
| Pressure-Temperature Rating | ASME B16.34 |
| Flanged Ends | ASME B16.5 (RF) |
| Face-to-Face Dimensions | ASME B16.10 (Long Pattern) |
| Inspection & Testing | API 598 / BS 6364 |
| Fire-Safe Design | API 607 / ISO 10497 |
| Anti-Static | Resistance < 10Ω (body-ball-stem) |
| Casting Material | ASTM A351 CF8 |
| Gear Operator Interface | ISO 5211 (Standard Pad) |
4. Main Technical Specifications
| Parameter | Value |
|---|---|
| Nominal Size | 6″ (DN150) |
| Pressure Class | Class 300 |
| Bore Type | Full Bore |
| Connection | Flanged RF per ASME B16.5 |
| Body / Bonnet Material | ASTM A351 CF8 (304 SS) |
| Ball Material | CF8 / SS304, Hard Chrome Plated |
| Seat Material | PCTFE (Kel-F®) |
| Stem Material | ASTM A182 F304 / F316 |
| Packing | Flexible Graphite / PTFE |
| Body-Bonnet Gasket | 304+Graphite Spiral Wound |
| Design Temperature Range | -196°C to +80°C |
| Extended Bonnet Length | ≥250 mm (from body centerline to packing base) |
| Leakage Class | Zero Leakage (BS 6364) |
| Operation | Manual Gear Operator with Handwheel |
| Design Features | Blow-out Proof Stem; Anti-Static Device; Cavity Relief |
5. Materials of Major Parts
| No. | Part Name | Material | Standard |
|---|---|---|---|
| 1 | Body | ASTM A351 CF8 | ASTM A351 |
| 2 | Bonnet (Extended) | ASTM A351 CF8 | ASTM A351 |
| 3 | Ball | CF8 / SS304, Chrome Plated | ASTM A351 |
| 4 | Seat Ring | PCTFE | — |
| 5 | Stem | A182 F304 / F316 | ASTM A182 |
| 6 | Packing | Flexible Graphite / PTFE | — |
| 7 | Body-Bonnet Gasket | 304+Graphite Spiral Wound | ASME B16.20 |
| 8 | Stud | A320 L7 (Cryogenic) | ASTM A320 |
| 9 | Nut | A194 Gr.4 (Cryogenic) | ASTM A194 |
| 10 | Antistatic Spring | SS316 | — |
| 11 | Gear Operator | Ductile Iron, Epoxy Painted | — |
| 12 | Handwheel | Carbon Steel (Painted) | — |
Note on PCTFE: PCTFE (Polychlorotrifluoroethylene), also known as Kel-F®, is the most widely specified cryogenic seat material in the industry. It maintains a tight seal at temperatures as low as -196°C and provides reliable sealing for LNG, liquid nitrogen, and other cryogenic media.
6. Principal Dimensions (6″ Class 300 RF)
| Symbol | Description | Value (mm) | Value (inch) |
|---|---|---|---|
| L | Face-to-Face Length | 356 | 14.02 |
| D | Flange Outside Diameter | 317.5 | 12.50 |
| D1 | Bolt Circle Diameter | 269.9 | 10.63 |
| D2 | Raised Face Diameter | 215.9 | 8.50 |
| b | Flange Thickness | 36.6 | 1.44 |
| f | Raised Face Height | 1.6 | 0.063 |
| n-Φd | Bolt Holes | 12 – Φ22.2 | 12 – 7/8″ |
| H | Center to Handwheel Top | Approx. 450~550 | Approx. 17.7~21.7 |
| Ext. Bonnet | Body Centerline to Packing Base | ≥250 | ≥9.84 |
| ISO 5211 | Top Mounting Flange | F10 / F12 | — |
| Weight (Approx.) | — | 60~85 kg | 132~187 lbs |
Note: Face-to-Face dimension per ASME B16.10 for Class 300 6″ flanged ball valves is 356 mm (14.02″). Extended bonnet length per BS 6364 for non-cold box applications is minimum 250 mm.
7. Cryogenic Treatment Process
All pressure-containing and sealing components are subjected to cryogenic treatment to ensure dimensional stability and prevent low-temperature embrittlement.
| Step | Description |
|---|---|
| 1. Rough Machining | Components are rough machined to near-final dimensions. |
| 2. Cryogenic Treatment | Parts are immersed in liquid nitrogen at -196°C for a specified duration (typically 1~2 hours). |
| 3. Natural Warming | Parts are removed and allowed to warm naturally to ambient temperature. |
| 4. Repetition | The cycle is typically repeated 2 times to ensure complete transformation of retained austenite. |
| 5. Final Machining | Precision machining of sealing surfaces (ball, seat pockets) is performed after cryogenic treatment. |
Purpose: Cryogenic treatment stabilizes the material structure, eliminates dimensional changes caused by retained austenite transforming to martensite, and ensures sealing fit precision at low temperatures.
8. Pressure Test Data
8.1 Ambient Temperature Tests (API 598)
| Test | Test Pressure (Class 300) |
|---|---|
| Shell Test | 7.7 MPa (77 bar) |
| High-Pressure Seat Test | 5.7 MPa (57 bar) |
| Low-Pressure Seat Test | 0.6 MPa (6 bar) |
8.2 Cryogenic Test (BS 6364)
| Item | Requirement |
|---|---|
| Test Temperature | -196°C (Liquid Nitrogen) |
| Test Method | Valve is submerged in a liquid nitrogen bath. Once at test temperature, the valve is pressurized and operated through open-close cycles. |
| Test Media | Helium gas (for leak detection) |
| Acceptance Criteria | Zero leakage at body, stem, and seat seals |
| Sampling | Minimum 10% of each type and size for valves operating below -55°C |
9. Impact Test Requirements (ASME B16.34)
| Material | Charpy V-Notch Requirement | Typical Performance |
|---|---|---|
| ASTM A351 CF8 | 18 J min (3-specimen avg.) / 14 J (single) at design temperature | CF8/CF8M castings typically achieve 60~100 J at -196°C, well above the minimum requirement |
Note: All cryogenic service materials must pass Charpy V-notch impact testing at the minimum design temperature or colder. Test specimens must be cooled to the design temperature prior to impact testing.
10. Gear Operator Specifications
| Parameter | Value |
|---|---|
| Type | Manual Worm Gearbox |
| Enclosure | IP67 (Standard) |
| Handwheel | Carbon Steel / Cast Iron |
| Output Torque | 300~600 N·m (typical for 6″ Class 300) |
| Mounting Flange | ISO 5211 F10 / F12 |
| Rotation | 90° (Open/Close) |
| Self-Locking | Yes |
| Options | Chainwheel, Electric Actuator, Pneumatic Actuator |
11. Design Features for Cryogenic Service
-
Extended Bonnet: Keeps packing and gland at ambient temperature, preventing seal failure and ice formation. Minimum 250 mm extension per BS 6364.
-
PCTFE Seat: Excellent low-temperature performance and chemical stability, suitable for long-term use at -196°C.
-
Cryogenic Treatment: Dimensional stability and prevention of low-temperature embrittlement.
-
Cavity Relief: Prevents abnormal pressure buildup caused by vaporization of trapped cryogenic liquid.
-
Anti-Static Device: Prevents static electricity accumulation in flammable media service.
-
Fire-Safe Design: Metal seat backup ensures sealing integrity in external fire conditions (API 607).
-
Blow-out Proof Stem: Prevents stem ejection under pressure.
-
Drip Plate: Prevents condensation from entering insulation (optional).
12. Applications
-
LNG liquefaction, regasification, and storage terminals
-
Air separation units (ASU)
-
Liquid oxygen, liquid nitrogen, and liquid argon systems
-
Ethylene storage and transportation
-
LPG and ammonia systems
-
Cryogenic rocket engine testing
13. Installation & Maintenance Notes
-
Installation Orientation: The valve should be installed with the extended bonnet vertically upward to keep the packing in the warmest possible position. Note the flow arrow on the body.
-
Insulation: The extended bonnet must be wrapped with cryogenic insulation (e.g., PIR/foam glass). The insulation should not cover the packing gland to allow for maintenance and inspection.
-
Flange Bolting: Use ASTM A320 L7 stud bolts and A194 Gr.4 nuts for cryogenic service. Tighten in a diagonal sequence to the torque specified in the IOM manual.
-
Operation: Cycle the valve slowly to avoid static electricity generation. Operating torque may increase slightly at cryogenic temperatures; this is normal.
-
Maintenance: Periodically inspect the packing gland for leakage. If leakage occurs, tighten the gland nuts evenly. Before returning to service after maintenance, re-perform cryogenic testing as required.
14. Ordering Information
To ensure correct supply, please specify:
-
Nominal Size: 6″ (DN150)
-
Pressure Rating: Class 300
-
Body Material: ASTM A351 CF8 / CF8M
-
Ball Material: CF8 / SS304 / SS316
-
Seat Material: PCTFE (Standard for Cryogenic)
-
Connection Standard: ASME B16.5 Class 300 RF
-
Operation: Gear Operator (Handwheel)
-
Cryogenic Test: BS 6364 (Required)
-
Special Requirements: (e.g., fire-safe, anti-static, NACE MR0175, oxygen cleaning)
Disclaimer: This data sheet is compiled based on visual inspection of the provided images and standard industry specifications for a 6″ Class 300 cryogenic floating ball valve. Exact dimensions, materials, and performance data may vary by manufacturer. Please confirm all critical parameters with the original equipment manufacturer (OEM) before procurement or installation.


